Custom Wafer Cleaning Systems: Tailored Solutions for Precision Semiconductor Manufacturing
2026-10-15
In semiconductor manufacturing, off-the-shelf cleaning tools often force compromises. When your wafer processes demand exact particle removal, specific chemical compatibility, or unconventional substrate handling, a generic system can stall your yield. That’s where Siansonic steps in. Our custom wafer cleaning systems are engineered from the ground up around your process parameters—not the other way around. From megasonic energy distribution to chemical delivery and robotics integration, every module is tailored to match your fabs’ precision requirements. This post explores how bespoke cleaning hardware eliminates variability, protects sensitive device structures, and shortens ramp-up times—without the usual over-engineering or hidden costs.
Cleaning Profiles Built Around Your Exact Stack
Most cleaning guides assume one universal routine, but your setup rarely matches the average. These profiles start with the tools and surfaces you already use—down to the specific attachments, finishes, and workflow order—so the settings feel familiar instead of forced.
When your countertop material, floor type, or appliance lineup changes, the profile adjusts in a way that mirrors how you actually move through the space. No digging through menus or overriding defaults. The sequence respects the order you clean, not a generic top-to-bottom checklist.
The result is less time spent correcting wrong modes and fewer passes over the same spot. You get a routine that fits the exact combination in front of you, without the extra noise.
Low-Damage Particle Removal That Holds Up in High Volume
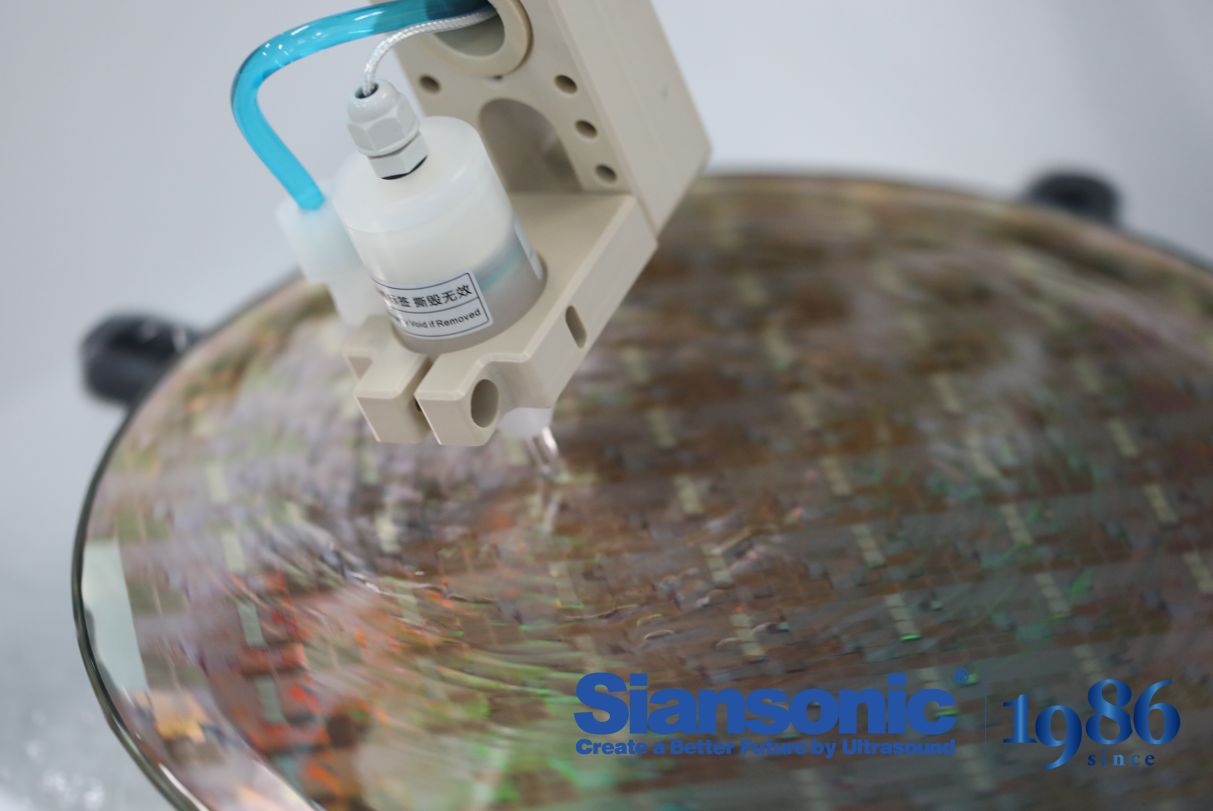
Removing sub-micron particles from delicate surfaces usually forces a choice: scrub hard enough to dislodge contaminants, or back off to avoid scratching the substrate. Most high-throughput lines pick the first option and accept a certain defect rate. The alternative described here takes a different route, using controlled micro-cavitation that collapses precisely at the particle-substrate interface. The energy is enough to break the adhesion force, but the pulse duration is so short that the underlying material never sees thermal or mechanical stress beyond a few nanometers of depth.
In a production environment, the real test is whether that gentleness survives when wafers or panels are moving past at a rate of hundreds per hour. Early prototypes worked beautifully on single samples but lost effectiveness once the conveyor speed increased, because the cavitation field could not re-form quickly enough. The fix came from redesigning the nozzle array and pulsing sequence so that each passing surface receives a staggered pattern of micro-jets. This lets the cleaning head maintain full coverage without dwell time, so a line running at 1.2 meters per second still gets the same particle removal efficiency as a static bench test.
Operators tend to be skeptical of any “low damage” claim until they see the post-clean defect maps. On a recent pilot run for silicon carbide wafers, the process held sub-0.1 defects per square centimeter while running 800 wafers per hour, with no measurable change in surface roughness. That kind of throughput, combined with a scratch-free finish, is what finally convinced the fab team to swap out their conventional brush scrubbers. The maintenance load also dropped, since there are no contact pads or brushes to wear down and replace every shift.
Wet Chemistry Tuned to the Nanometer
Achieving true nanometer-scale control in wet chemistry hinges on manipulating reaction kinetics far below the limits of conventional stirring and heating. It is not enough to mix precursors and wait; one must choreograph nucleation and growth as separate events. By rapidly injecting a reactive species into a hot solvent, for instance, you can force a burst of homogeneous nucleation that starves the solution of monomer, allowing the existing seeds to grow uniformly rather than spawning new particles. The temperature drop, the ligand coverage, and even the stirring speed all become dials that move the average particle diameter by fractions of a nanometer.
Seed-mediated approaches take this further, decoupling nucleation from growth entirely. Small, well-defined seed particles are introduced into a growth solution where additional precursor is reduced onto their surfaces under mild conditions. Here the shape is not dictated by thermodynamics alone but by the relative stability of different crystal facets in the presence of specific capping agents. A slight excess of silver ions, a particular halide, or a trace of polymer can switch the final product from spheres to cubes, rods, or branched structures — each with dimensions controlled to within a few atomic layers.
The practical payoff appears in optical and electronic properties that shift dramatically over just one or two nanometers. A cadmium selenide quantum dot emitting green light versus red light may differ by less than a nanometer in radius, and that difference is set almost entirely by the temperature profile and precursor concentration during the first seconds of reaction. While batch-to-batch reproducibility remains a challenge, recent work with microfluidic reactors and in-situ spectroscopy is closing the loop between measurement and adjustment, letting chemists correct growth trajectories in real time rather than relying on recipes.
Modular Systems That Grow With Your Fab
Most fabs hit a wall when a new process step demands tools that were never part of the original floorplan. Modular systems sidestep this by treating each subsystem—load ports, transfer chambers, process modules, even the gas and chemical delivery panels—as a self-contained unit that can be added or rearranged without tearing down the cleanroom around it. You might start with a two-chamber etcher, then bolt on a third chamber and a different endpoint detector six months later, reusing the same frame, vacuum pumps, and safety interlocks.
What makes this approach practical is that the interfaces are defined before you need them. Power drops, exhaust ducts, and drain lines get pre-positioned along the tool’s spine, and the control software already knows how to address a module that isn’t physically installed yet. A furnace stack, for example, can accept an extra tube as demand grows, while a wet bench can take another rinse-dry station without rewriting the recipe management system. The fab's automation host sees the new module as just another addressable endpoint.
There are limits, of course—modular doesn’t mean infinite. But the real advantage shows up during ramp cycles and technology transitions. Instead of buying a bigger tool and hoping the process still translates, you extend the one you have, preserving the qualification data and the operators' muscle memory. That’s why many fabs now ask vendors for frame layouts with spare slots and pre-tested expansion kits, even if they never plan to use them all. The empty slot costs a little more upfront; the alternative usually costs a lot more later.
Process Transparency Without the Data Overload
Most teams don't actually need another dashboard. What they need is a clear line of sight into how work moves without being buried under a dozen metric cards. Process transparency works best when it surfaces the few signals that matter at the right moment, rather than forcing everyone to sift through raw event logs or weekly status decks.
A practical way to strike this balance is to map the major stages of a workflow and highlight only where items tend to stall or loop back. Instead of showing every touchpoint, show the exceptions that deserve attention. This gives stakeholders enough context to trust the process without turning every review into a forensic audit.
The goal is not to expose every detail but to make the invisible handoffs visible. When people can quickly see who is waiting on what, the conversation shifts from defending status to resolving friction. That is the kind of transparency that reduces meeting load instead of adding to it.
From Bevel to Backside, Nothing Left to Chance
Every edge starts with an argument between metal and hand. The bevel gets ground, checked against light, then ground again until it reads like a clean sentence. No shortcuts, no presuming the jig stayed true overnight.
Flip the piece over and the backside tells the rest of the story. Flatness matters more than polish, so we lap it on glass with progressively finer grit until a shadow cannot hide anywhere. If a low spot survives, the whole blade goes back to the stones.
That loop—bevel, backside, bevel again—continues until both faces agree. Only then does buffing start, and even that gets measured, not eyeballed. Nothing leaves the room on a maybe.
FAQ
Standard tools force you to adapt your process; a custom system is built around the exact substrate material, contamination profile, and throughput targets your line already has. That means chamber geometry, chemical delivery, and drying methods are selected to match your reality instead of a generic datasheet.
They focus on repeatable control at every stage—temperature, flow rate, megasonic energy, and rinse timing are tuned to the specific film stack and feature size. The goal is removing defects without introducing new ones, so tolerances are held much tighter than in general-purpose cleaners.
Most custom platforms can be designed for 100mm to 300mm wafers, and some extend to 450mm or non-standard substrates like silicon carbide, gallium nitride, or glass. The key is that the handling and chemistry are validated for your exact wafer type, not just the most common silicon CMOS flow.
That depends on the tool layout. Options include dedicated chemistry loops for each process family, segregated drying modules, or automated purge sequences between recipes. The customization phase identifies which approach fits your floor space, chemical budget, and risk tolerance.
Yes, but it requires early planning. Interface points like load ports, SECS/GEM communication, and exhaust or DI water connections are matched to your current infrastructure. Some fabs phase in the new system by running non-critical lots first, which keeps the line moving while process engineers validate performance.
Drying is often the step that determines final yield. Custom systems may use IPA vapor dry, Marangoni-style drying, or heated nitrogen depending on the feature geometry and material sensitivity. The choice is made after testing on your actual patterned wafers, because a method that works for blank silicon can leave residues on high-aspect-ratio structures.
Validation typically involves running split lots with your own test vehicles, measuring particle counts, metal contamination, and surface roughness before and after cleaning. The acceptance criteria are agreed upon with your process team, so the system is not signed off until it meets your specific defect density targets.
If your process is already near the edge of its defect budget, a standard tool may force compromises in chemistry or handling that cost more in yield loss than the price difference. A custom system pays off when it removes a persistent defect class, reduces rework, or enables a new material that standard platforms cannot support safely.
Conclusion
Custom wafer cleaning systems address the exact film stacks, pattern densities, and surface sensitivities of each device architecture. Rather than forcing a standard recipe, engineers map cleaning profiles around the stack itself—adjusting chemical exposure, megasonic energy, and rinse protocols for fragile low-k dielectrics, high-aspect-ratio trenches, or metal gates. The result is low-damage particle removal that keeps defect counts flat even when throughput climbs into high-volume manufacturing. Wet chemistry is tuned to the nanometer: dilutions, pH, and additive packages shift to remove residues without etching critical dimensions, while inline sensors confirm every bath stays within spec.
These systems are built as modular platforms, so a benchtop tool can grow into a fully automated cluster as fab capacity expands—add chambers, robots, or chemical delivery modules without ripping out the cleanroom floor. Process transparency comes from a curated dashboard: not raw log files, but a live summary of particle removal efficiency, chemical lifetime, and wafer-to-wafer variation that flags drift before it becomes yield loss. Coverage extends from bevel to backside, with dedicated nozzles, edge-grip handling, and backside scrub modules ensuring no surface is left to chance. That combination of tailored chemistry, scalable hardware, and focused data turns cleaning from a generic step into a precision process step matched to each product node.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/