Best Kraftformer Manufacturing in China for Precision Metal Forming Solutions
2026-09-16
Most Kraftformer buyers start with a simple question: can a Chinese-built machine really hold tolerance on complex panels? JIAN MENG answers it every day—by building precision metal forming solutions that rival the best imports, without the import price tag. Here’s why that matters for your next forming project.
Why Chinese Kraftformer Builders Are Gaining Ground in Precision Forming
A decade ago, most precision forming shops looking for a Kraftformer-style machine would have defaulted to established European names. Chinese builders were often dismissed as copycats with loose tolerances and rough castings. That perception has quietly shifted. Many manufacturers now run in-house calibration labs, use higher-grade spindle bearings, and pay far more attention to ram alignment and slideway scraping than they did even five years ago. The result is repeatability and surface finish that no longer embarrass a shop owner when a customer audits the line.
The real pull, though, is practical: shorter lead times and direct access to factory engineers. When a part geometry changes or a tooling interface needs modification, a Chinese builder can often redesign the ram guide or stroke control within weeks, not months. That responsiveness matters in job shops where downtime is expensive and a standard catalog machine won't do the job. It's not unusual to have a WeChat conversation with the actual design engineer, mark up a drawing, and get a revised quote the next morning.
Price remains a factor, but it is no longer the only one. Buyers are realizing that mid-range Chinese Kraftformers can hold ±0.02 mm on small batches while costing 40–60 percent less than comparable European units. Add readily available spare parts, bilingual documentation, and a growing network of service technicians in North America and Europe, and the value proposition becomes hard to ignore. For shops that need a capable machine without the premium brand markup, Chinese builders are no longer the risky option they used to be.
What Actually Limits Accuracy in a Standard Kraftformer
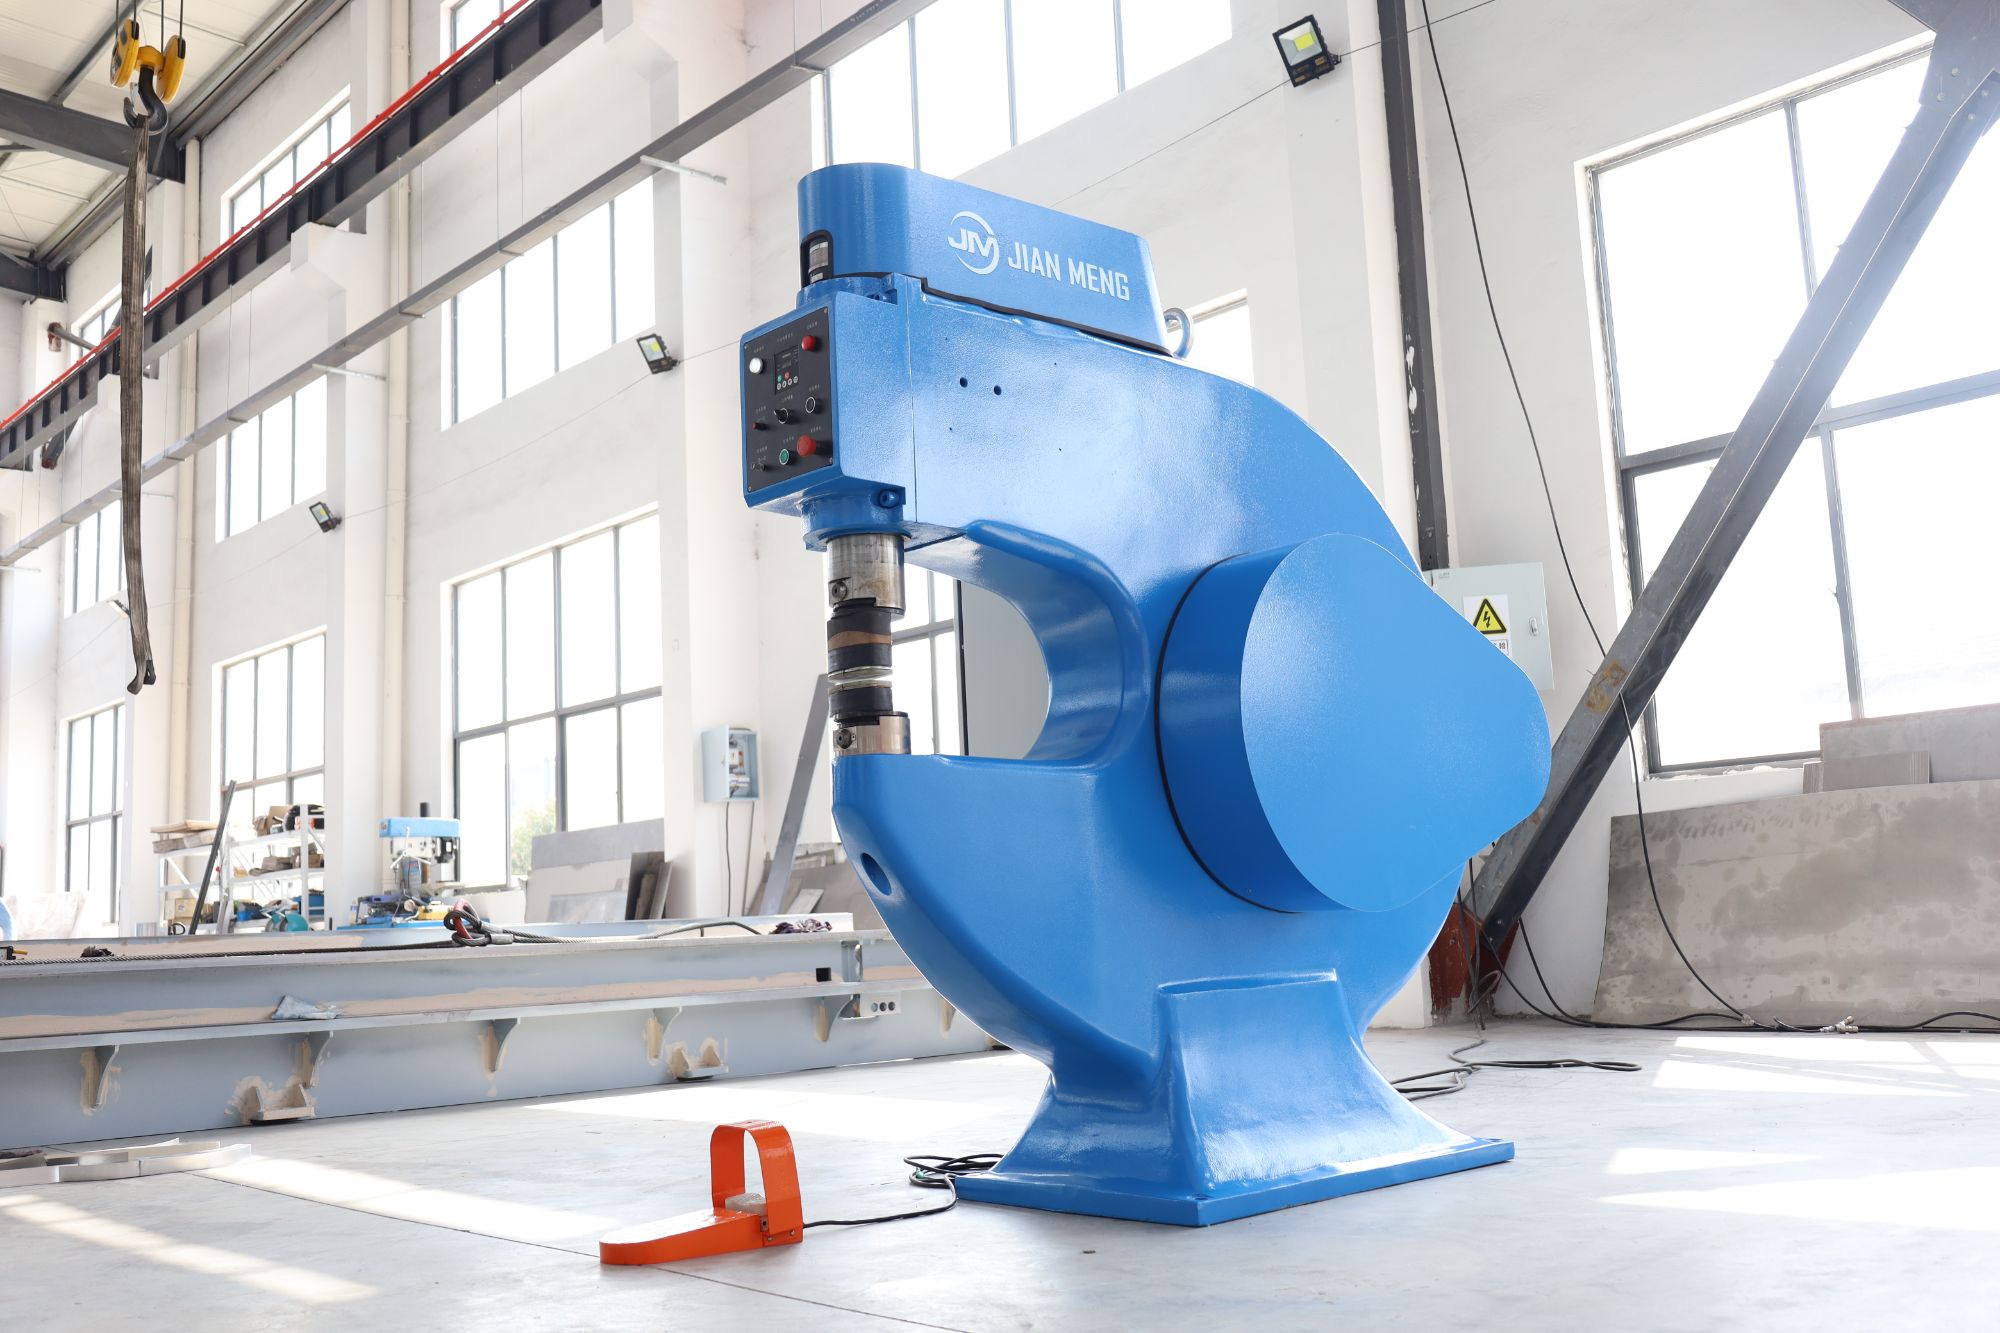
On a standard Kraftformer, the first real cap on accuracy is structural flex in the open C-frame. Even with a well-adjusted ram, the throat deepens under heavy forming loads, and that elastic deformation tilts the upper die just enough to shift the contact line. Once the machine has a few thousand cycles on it, the plain gib ways start to show localized wear, so the same stroke setting no longer repeats to the same position every time. You can shim and re-scrape the ways, but without a closed frame or preloaded guides, there's always a small, load-dependent drift.
Material behavior is the second limit that gets blamed on the machine. Sheet stock from different coils can vary in yield strength and thickness enough that the same tool path produces visibly different flange angles. Grain direction matters too—forming across the grain gives more springback than forming along it. A standard Kraftformer has no sensor loop to measure actual bend angle or part springback after the hit, so the operator has to compensate by feel, sneak up on the final shape, or run extra test pieces whenever a new batch arrives.
The third constraint sits between the handwheel and the tooling: open-loop depth control. Most standard Kraftformers rely on mechanical stops and the operator's judgment for stroke depth, dwell time, and repeat hits. There is no live feedback telling the control system that the part has moved, thinned, or slipped in the clamps. Small changes in lubrication, blank positioning, or even ambient temperature can change friction and forming resistance enough to push a dimension outside tolerance. Until you add closed-loop measurement or at least a digital readout tied to the ram, the machine can only repeat what it is told, not correct what it is doing.
The Metal Flow Details Most Kraftformer Specs Never Mention
A Kraftformer’s spec sheet will tell you tonnage, stroke length, and maybe the range of tooling shanks it accepts. What it won’t mention is how the sheet actually flows when the forming head tilts a few degrees off perpendicular. On most machines, metal moves in a shallow wave ahead of the contact point—compression builds, then releases as the workpiece rotates. But on a well-tuned Kraftformer, that wave is asymmetric: the upper die drives material downward and inward more than the lower die pushes it back, which gives you a tighter radius without thinning the outside wall. You can feel the difference as a slight drag in the handwheel about two-thirds through the stroke, right before the metal settles.
That drag is where operators either learn to back off the pressure or start fighting the machine. If you keep feeding at the same rate, the material folds into micro-pleats that later show up as surface ripples after planishing. The fix is not more tonnage—it’s letting the workpiece coast for a few degrees of rotation so the compressive zone can redistribute. Think of it like pushing a puddle of cold syrup with the edge of a spoon: too fast and the syrup bunches; too slow and you lose the wave entirely. The sweet spot varies with material thickness and alloy, but it’s rarely in the manual.
Another detail specs omit is the return stroke’s effect on grain structure. On cheaper machines, the tooling snaps back and momentarily loses contact, which lets the partially formed flange spring outward. A properly adjusted Kraftformer maintains light contact through the entire return, burnishing the inner radius as the dies separate. That burnish line—visible as a subtle bright streak on mild steel—is a quick field check for whether the machine’s linkage is still within tolerance. If the streak fades on one side, you’ve got eccentric wear in the pivot, not a pressure problem.
How Small Shops Use Kraftformers for Prototype Metal Parts
Small shops often reach for a Kraftformer when a prototype metal part needs a gentle curve, a crisp flange, or a subtle offset. Instead of waiting on outsourced stamping dies, a machinist can clamp a piece of 18-gauge steel into the machine’s jaws and work the lever by hand. The slow, controlled squeeze lets you sneak up on the exact bend angle without over-forming the blank. Many shops keep a set of custom-made nylon or hardwood tooling nearby, swapping shapes in minutes to match a sketch or a cardboard template.
The real advantage shows up during design iterations. A bracket might need a half-inch more kick on one leg, or a mounting tab has to tilt three degrees to clear a bolt head. With a Kraftformer, you mark the new line, adjust the lower die height, and rework the same piece until it fits the mating part. There’s no programming, no toolpath simulation—just the feel of the metal giving way under pressure. Some shops even use it to soften laser-cut edges or add a slight crown to a flat panel, things a press brake struggles to do without dedicated tooling.
For prototype runs under a dozen parts, this manual approach beats sending files to a stamping house. One machinist described making a dozen aluminum heat shields in an afternoon, each one tweaked by hand until the customer’s assembly inspector nodded. The finished parts don’t carry the polished look of production tooling, but they prove the form, fit, and function before any hard tooling budget gets approved. And when the design shifts again—as prototypes always do—the Kraftformer sits ready, no die changeover forms to fill out.
Where to Look for Real Quality Signals in Kraftformer Manufacturing
Start with the parts that never show up in glossy photos. Pull a side cover and look at the inside of the main casting. A quality Kraftformer builder will leave the as-cast surfaces free of filler and excessive paint, because stress relief and clean foundry work are visible there. Check for uniform wall thickness around the forming head pocket and look for machined pads at every bolt-up point. If the frame has been thermally stress-relieved, ask for the furnace chart, not a verbal promise.
The tooling interface tells you more than the spec sheet. Loosen and retighten a die holder a few times and watch how the taper or clamping surfaces repeat. Look for hardened thrust washers, bronze wear strips that can be shimmed, and dowel pins in locations that actually carry shear load, not just alignment. Run the ram through its full stroke by hand if possible; any tight spot near mid-stroke usually means a bent guide or a poorly finished gib.
Pay attention to how the manufacturer handles service data. Real quality shows up in a manual that lists specific torque values for the tie rods, wear limits for the main bearings, and a defined procedure to measure ram-to-table parallelism. Ask for the recommended oil cleanliness class and filter micron rating. If they offer a laser alignment report with each machine or include part numbers for every wear component, that is a stronger signal than a long warranty paragraph.
Custom Kraftformer Tooling and Its Impact on Complex Geometries
Off-the-shelf Kraftformer tooling often struggles when a part calls for tight radii, deep draws, or abrupt changes in cross-section. Custom tool sets address this by matching the die contours to the exact profile of the workpiece, which spreads the forming load more evenly. Instead of forcing the metal into a generic shape and then fighting springback, the tool itself guides the material along a controlled path. That means less thinning at the corners and fewer secondary operations to correct distortion.
Complex geometries also benefit from how custom tooling handles localized strain. A standard rounded punch tends to push material outward uniformly, but real parts rarely need that. With a tailored upper and lower die, you can concentrate deformation where the design calls for it—sharp creases, offset flanges, or blended radii—while leaving adjacent areas relatively undisturbed. The result is a more predictable grain flow, which translates into better fatigue resistance and a finished surface that needs minimal hand finishing.
From a practical standpoint, investing in custom Kraftformer tooling changes the way a shop approaches difficult jobs. Instead of rejecting or heavily modifying a drawing because the standard tool can't cope, engineers can plan around the exact tool geometry from the start. Setup time drops because less trial-and-error is needed to hit the correct shape. And for repeat production runs, the custom tool pays for itself by cutting scrap rates and allowing tighter tolerances on parts that would otherwise be considered borderline formable.
FAQ
Kraftformers combine spinning and pressing motions to let operators control material flow in small increments. This reduces springback and thinning, especially on complex shapes like cones, hemispheres, and flanged parts. Conventional presses often need dedicated tooling for each profile, while a Kraftformer can handle multiple geometries with interchangeable rollers and mandrels.
Several Chinese builders have invested heavily in CNC machining and heat treatment for the main frame and tooling, which closes the gap with older European designs. They also tend to offer quicker customization cycles and more flexible spindle configurations without the long lead times often seen with imported machines.
Look at the machine's frame rigidity, spindle runout, and the range of feed rates. Also ask for sample runs on your actual material grade—aluminum, stainless, or copper behave differently, and a builder who can show measured thickness distribution across a formed part is usually more reliable than one who only quotes maximum blank diameter.
Tooling geometry determines how the metal is progressively worked; a well-designed roller set can move material without creating wrinkles or excessive local thinning. Some manufacturers provide simulation or at least trial-run validation to refine roller paths before finalizing the tooling, which matters more than the machine's raw power.
They show up in lighting fixtures, cookware, ventilation parts, musical instruments, and automotive prototypes. Many job shops use them for low- to medium-volume production where the part shape changes often and hard tooling would be too expensive or slow to modify.
In many cases yes, especially when you need deep, seamless shapes or frequent design changes. It won't match the per-piece speed of a transfer press for very high volumes, but it avoids the cost of dedicated dies and allows in-process adjustments that are hard to do with stamping.
The best ones have in-house metallurgy know-how for rollers and mandrels, plus experience with servo or hydraulic feed systems that respond smoothly under load. They also document spindle alignment and offer calibration support after installation, rather than treating the sale as a one-time transaction.
Typically these machines handle blanks from roughly 0.5 mm up to 8 mm in steel, and diameters from 200 mm to 1600 mm depending on the frame size, but limits vary by builder. Always confirm the maximum blank diameter at the actual thickness you plan to run, because capacity charts based on thin aluminum can be misleading.
Conclusion
Chinese kraftformer builders have moved well past copying older European designs. The real shift happens in how they handle frame rigidity, ram alignment, and the small adjustments that keep sheet metal from thinning unevenly. Shops that once struggled with standard machines now get repeatable strokes because builders pay attention to gib fit, slide clearance, and the way force travels through the tool holder. That matters more than most catalog specs suggest. In a typical kraftformer, the deepest accuracy problems come from play in the pivot points and slight flex in the C-frame under load, not from the motor or the stroke length. Several workshops now use the machines for prototype panels and brackets, working from CAD files to hammer out one-off parts without spending on stamping dies. The result is a faster loop between design and a usable metal sample.
Metal flow is the hidden variable in every forming job. A standard specification sheet rarely tells you how the sheet will stretch or gather near a deep radius, so builders compensate with custom tooling and controlled dwell. The better manufacturers machine their own upper and lower blocks, match radii to the material thickness, and adjust the hammering frequency to avoid work hardening too fast. When you look for real quality signals, check whether the factory heat-treats the tool holders, inspects the ram bore alignment, and keeps spare anvils in stock. Small shops use these same details to hold tolerances on complex geometries that would be expensive to stamp. Custom tooling makes a visible difference in how cleanly a corner forms and whether the part needs hand finishing afterward. That practical focus—rather than glossy brochures—is what separates the competent Chinese builders from the rest.
Contact Us
Contact Person: Jeanie
Email: [email protected]
Tel/WhatsApp: +86 19805122954
Website: https://www.jianmeng.com