Best HDPE Pipe Production Line Features You Should Evaluate
2026-10-26
Most HDPE pipe line comparisons stop at output rate and pipe diameter. That's exactly where costly surprises hide. The real difference shows up months later — in wall thickness variance, scrap rates, energy per meter, and how fast your crew can switch sizes. If you're evaluating production lines for a new plant or an upgrade, your checklist needs to go deeper than brochure numbers. COMRISE builds lines with those overlooked details in mind. Here are the features worth your time.
Extruder Output That Stays Consistent When You Push It
Most extruders behave fine on paper, but the real test comes when you apply pressure by hand or through a filament runout sensor. A well-designed drive train keeps the filament engaged without slipping, so the output stays even whether you're feeding slowly or giving it a firm push. That means no sudden under-extrusion just because the spool tension changed or you nudged the filament during a swap.
Temperature stability in the melt zone matters just as much as the mechanical grip. If the heat block cycles too widely, the plastic softens unevenly and the same push produces a thicker or thinner strand. Good thermal regulation and a short, constrained path from the drive gear to the nozzle help translate your input into a steady bead instead of a pulsing one.
What separates a dependable extruder from a frustrating one is how it handles low-speed starts and mid-print adjustments. You can feel the difference in the consistency of the extruded line: no stretching, no intermittent blobs, just a continuous thread that matches the pace you set. That predictability matters whether you're calibrating flow rate or manually advancing filament for a color change.
Die Head Geometry That Avoids Weld Line Weak Spots
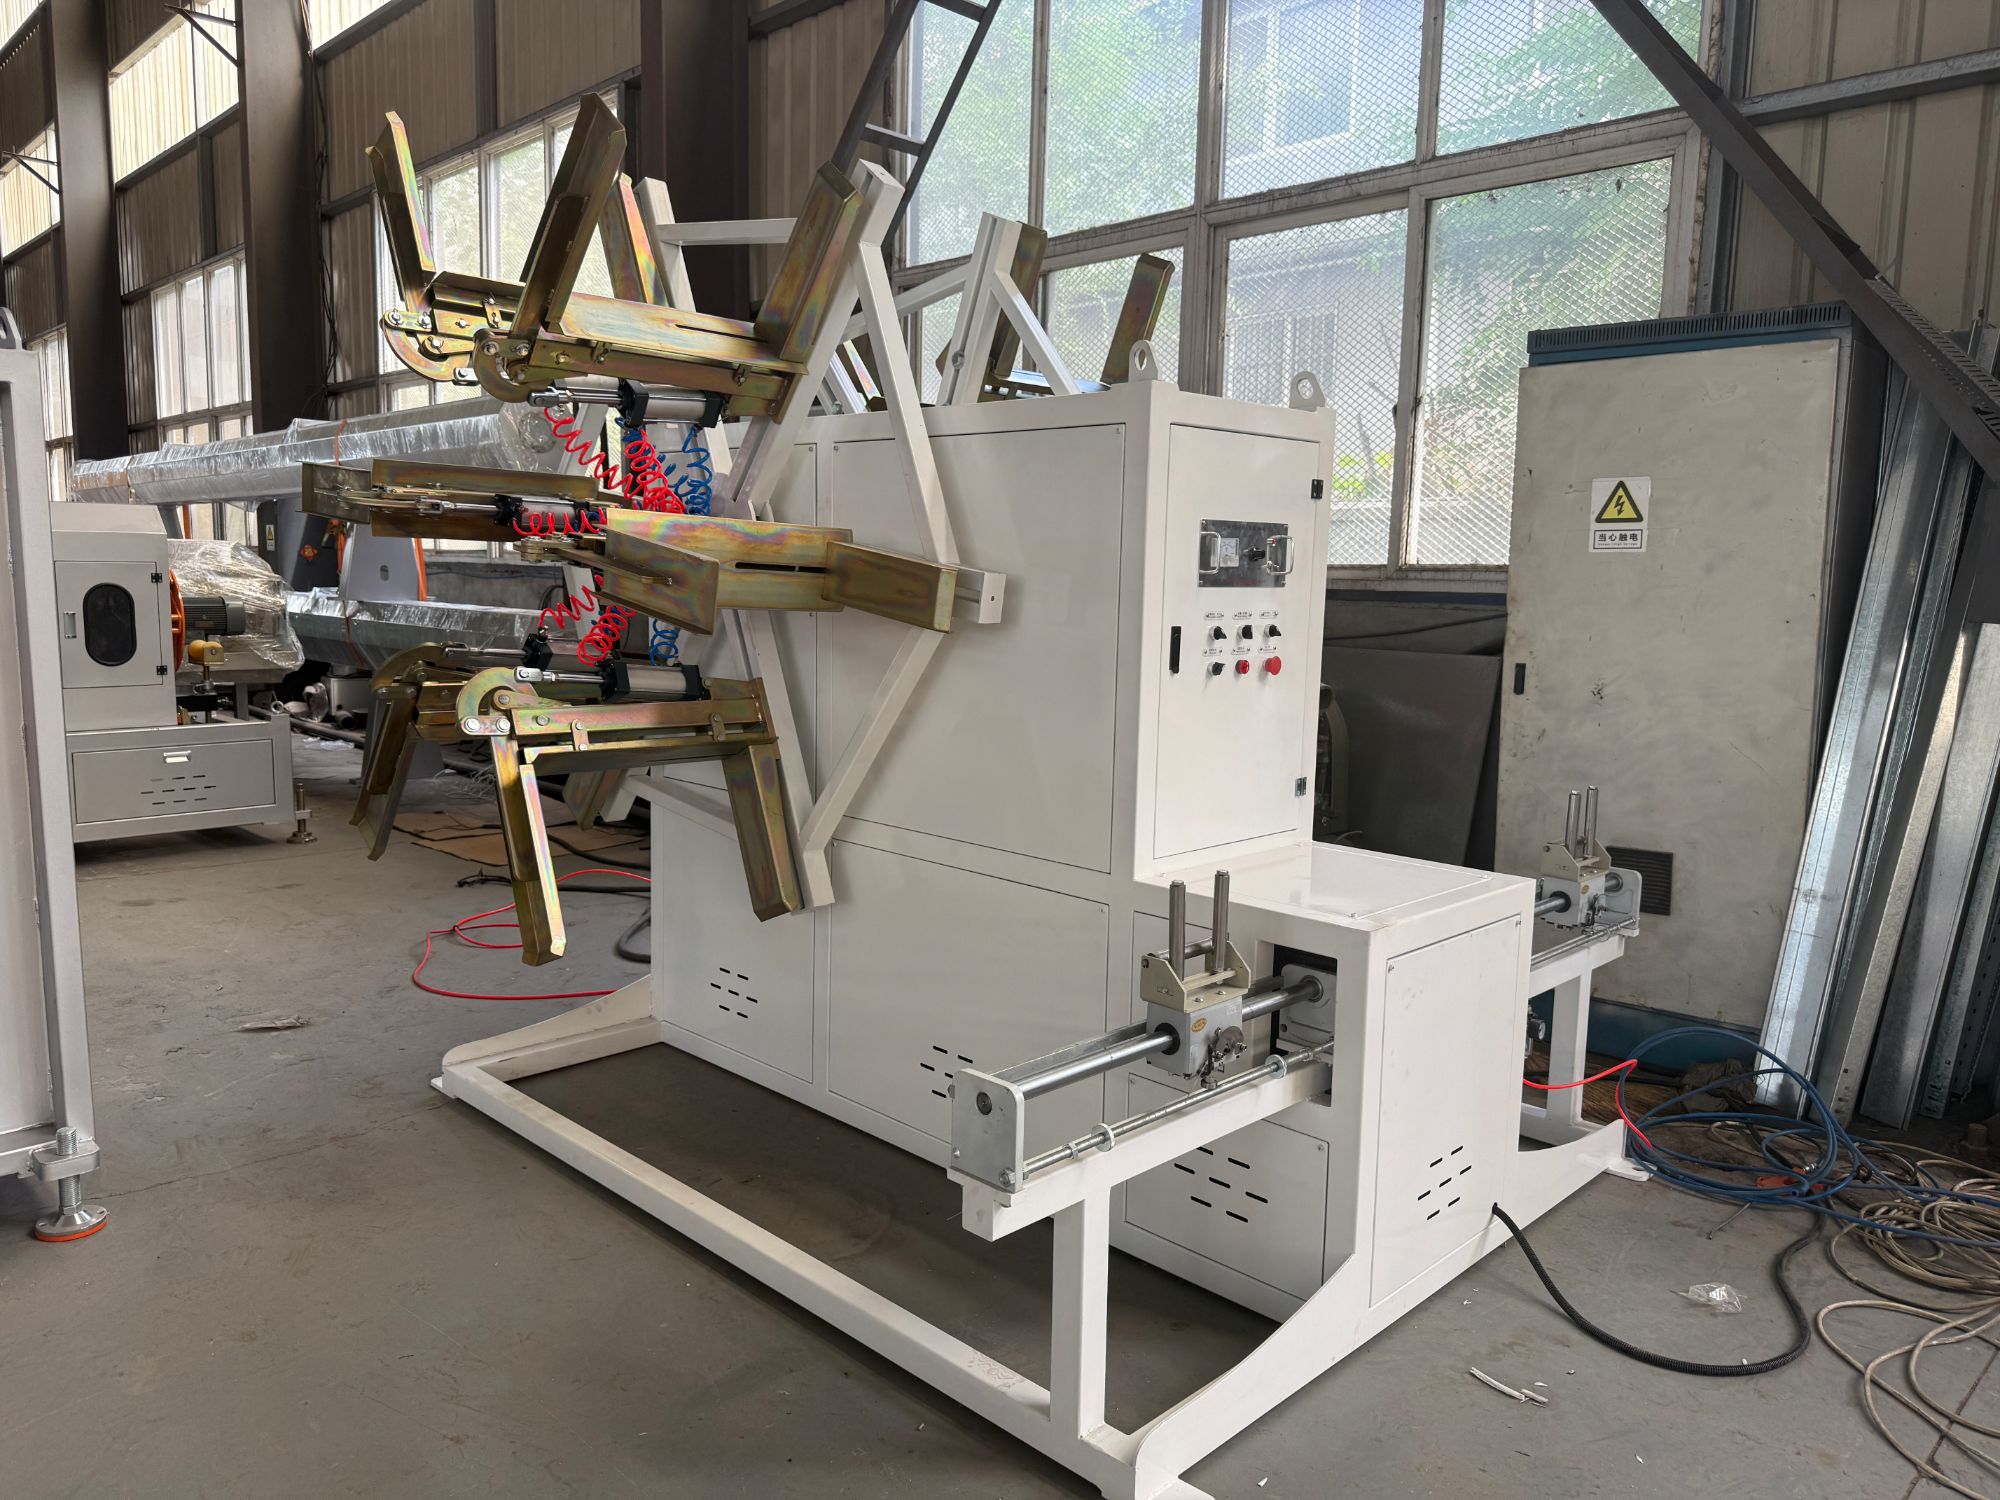
The geometry of a die head plays a decisive role in how molten polymer streams reunite after flowing around the mandrel. Weld lines form where these separate melt fronts meet, and their mechanical strength often drops below the surrounding material. By adjusting the convergence angle and using spiral or heart-shaped flow channels, engineers can shift the meeting point away from high-stress regions. A longer, tapered land area gives the polymer more time to relax and entangle across the interface, turning a sharp knit line into a diffuse, load-bearing junction.
One practical approach is to offset the mandrel tips or introduce a slight spiral twist in the distributor, which rotates the melt fronts so they overlap at a shallow angle instead of butting head-on. This forces the polymer chains to interpenetrate across a broader zone. Some die designs also incorporate a local temperature-controlled zone just downstream of the weld region, keeping the polymer above its crystallization temperature a bit longer. The extra thermal energy allows chain diffusion to heal the interface before solidification locks in a weak plane.
Manufacturers who struggle with split parisons or burst pressure tests often find that a small change in land length or a reshaped torpedo reduces weld-line depth significantly. Rather than chasing material additives or higher melt temperatures, which can cause degradation, modifying the internal flow path targets the root cause. A properly contoured die head can boost weld strength by 20 to 40 percent in many polyolefin and engineering resin applications, all without adding cycle time or secondary operations.
Vacuum Calibration Sleeves Designed for Fast Size Changes
Swapping extrusion line tooling usually means shutting down, wrestling with hot parts, and losing valuable run time. These vacuum calibration sleeves flip that script. The design focuses on quick-change geometry, so operators can pull one sleeve and lock in a different profile size in minutes instead of hours. There is no need to recalibrate the entire vacuum tank or break out special alignment jigs.
What sets them apart is the attention to material and surface finish. The sleeve walls hold tight tolerances across repeated thermal cycles, which keeps the vacuum seal consistent from size to size. Because the interlocking mounting points are machined rather than bolted through soft spots, you avoid the usual air leaks that cause scoring or uneven cooling. A single operator can handle the swap, and the reduced downtime tends to show up on the production sheet within the same week.
Cooling Sections That Pull Heat Without Wasting Water
Most cooling setups treat water as something to burn through, but the newer sections flipping that script rely on clever airflow design and phase-change materials instead of open evaporation. They pull thermal energy away from process lines using finned coil arrays and a sealed coolant loop, so the only thing leaving the stack is warm air.
What makes these sections feel different is how they handle peak loads. Rather than drenching pads or spraying mist, they cycle a glycol mix through micro-channel plates that shed heat into a dry air stream. The result is a system that holds a steady discharge temperature even when ambient conditions swing, without a single drop going down the drain.
Operators who switch over often notice the maintenance shift first: no basin to scrub, no mineral buildup on louvers, and no water treatment logs to keep. That quiet drop in upkeep, plus the fact that cooling capacity stays predictable, tends to win people over more than any spec sheet claim.
Haul-Off and Cutter Sync That Eliminates Stop-Start Jitter
Synchronizing the haul-off and cutter eliminates the jerky motion that often plagues extrusion lines when they pause between cuts. Instead of relying on a stop-start cycle, the system continuously adjusts the puller speed to match the cutter's blade position, creating a smooth, uninterrupted flow. Operators notice the difference immediately: the product emerges with consistent wall thickness and surface finish, while the line runs quieter and with less wear on mechanical components.
The key lies in a closed-loop control that reads the cutter's rotational phase and feeds it forward to the haul-off drive. As the blade approaches the cut point, the puller momentarily slows just enough to allow a clean sever, then instantly resumes its set speed—without ever dropping to zero. This approach avoids the lurching that causes dimensional variations at the cut ends and reduces scrap, especially on thin-wall tubing or fragile profiles.
For line operators, the benefit is predictability. Start-up jitter becomes a thing of the past, and the cut length accuracy improves because the synchronization compensates for inertia in real time. Maintenance intervals stretch out too, since the absence of hard stops spares belts, bearings, and gearboxes from shock loads. The result is a line that feels planted and steady, even at high throughput.
Control Panel Logic You Can Actually Diagnose at 2 a.m.
Most control panel failures stop being mysterious once you ignore the schematic for five minutes and trace where the enabling signal dies. At 2 a.m., a meter and a flashlight beat a laptop. Check the e-stop loop first: one loose wire at a door interlock can hold out an entire sequence, and it will look fine until you wiggle it.
Relay logic panels have their own quiet hierarchy. If the power supply LED is on but nothing pulls in, look for a missing neutral return on the control transformer, or a fuse that's blown only under load. Swap the suspect relay with a known-good one from an unused circuit instead of guessing from coil resistance; heat-related intermittent contacts show up better that way.
For PLC-driven panels, don't rebuild the program at that hour. Force a single output from the HMI or laptop and listen for the contactor. If the output LED lights but the contactor doesn't move, the problem is downstream: a broken wire, a dead coil, or a tripped motor starter overload. Write down exactly which rung stopped, then go fix the mechanical side first.
FAQ
Look beyond the extruder size. A high-output line pairs a 33:1 L/D barrier screw with a grooved feed section, and the downstream must handle the increased melt volume without bottlenecking. You'll see differences in vacuum tank length, cooling water flow rate, and the puller's contact area.
For HDPE, a barrier screw with a mixing section handles different melt indexes and recycled content better than a standard metering screw. The grooved feed throat stabilizes output even when bulk density shifts, which matters if you switch between virgin and regrind.
The vacuum level should hold between -0.03 and -0.05 MPa, and water temperature should stay within 15–20°C for consistent cooling. The number of spray jets and their angle also matter more than tank length alone—poor jet distribution creates ovality even with long tanks.
Use a caterpillar puller with at least six contact points and pneumatic pressure adjustment. The pad material should be polyurethane, not rubber, to reduce marking. Also verify the speed synchronization range—if the puller can't match the extruder output smoothly below 0.5 m/min, start-up scrap rises sharply.
Usually yes. It removes guesswork when running multi-layer or foamed core pipes, and it keeps the melt pressure steady if your feedstock varies between batches. Without it, you'll see more thickness drift, especially at line speeds above 10 m/min.
An ultrasonic wall thickness gauge that feeds data back to the control system can adjust haul-off speed automatically. A melt pressure sensor before the screen changer also alerts you before a blockage affects output. Skip lines that only log data without closed-loop correction—they don't pay back.
Check if the line uses AC motors with variable frequency drives on the extruder, puller, and vacuum pump. Barrel heaters should be divided into at least six zones with ceramic insulation. Compare specific energy consumption (kWh/kg) at your target pipe diameter, not just installed power.
Emergency stop cords along the full cooling and haul-off length, interlocked guards on the cutter, and a centralized lubrication system. Also look for quick-release die heads and swing-out haul-off tracks—they cut die change time from hours to under 30 minutes.
Conclusion
When you're comparing HDPE pipe extrusion lines, the glossy brochure will gladly list maximum output, but the number that matters is the output the extruder holds under real load. A screw and barrel that surge or overheat when pushed to rated speed will create wall thickness variation you'll chase all shift. Equally important is the die head geometry—poorly designed flow channels leave weld lines where the melt fronts meet, and those weak spots can fail under pressure years later. Then consider how the vacuum calibration sleeves are built. If a size change requires excessive disassembly or fragile alignment, the line's flexibility is more theoretical than real, and your operators will dread every diameter switch.
Thermal control and motion synchronization decide whether the line runs quietly at night or keeps someone babysitting it. Cooling sections should pull heat out fast without flooding the floor or sending thousands of liters down the drain; efficient water use is a cost issue, not just an environmental one. The haul-off and cutter need to work as one unit—any lag or jerk between them shows up as surface marks, ovality, or cut length drift, and those defects are expensive to sort later. Finally, pay attention to the control panel logic. At 2 a.m., a clear fault trace on the screen can save you from a costly shutdown, and it tells you whether the machine builder actually thought about how the line will be operated, not just assembled.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com